In heavy-duty industries such as mining, water well drilling, and infrastructure construction, the operational reliability of pneumatic equipment directly dictates project timelines. Within a reciprocating piston air compressor, the valve assembly represents the heart of the compression cycle. These components continuously regulate the high-frequency intake and discharge of air columns; thus, any minor valve anomaly can rapidly cascade into reduced volumetric efficiency, excessive thermal generation, heightened fuel or power consumption, and eventual mechanical seizure.

As a leading global industrial equipment manufacturer specializing in integrated research, manufacturing, and trade, Quzhou Zhongdu Machinery Technology Co., Ltd. (Moderate Machine) engineers robust piston systems capable of enduring the most punishing field environments. In this technical guide, we will analyze the functional mechanics of piston compressor valves, outline rigorous maintenance protocols, and demonstrate how proper valve optimization aligns with long-term cost-effectiveness.
Technical Mechanics: Intake vs. Discharge Valves
To establish an effective preventative maintenance framework, field engineers must first isolate the distinct mechanical behaviors of the two primary valve categories:
1. Intake (Suction) Valves
Intake valves manage the introduction of ambient atmospheric air into the compressor cylinder during the downward piston stroke. Operating under a differential pressure mechanism, these spring-loaded reed or disc valves snap open the moment the internal cylinder pressure drops below ambient atmospheric threshold. If an intake valve fails to seal completely during the return stroke, compressed air leaks back into the atmosphere, causing severe volumetric losses.
2. Discharge (Delivery) Valves
Discharge valves control the evacuation of highly compressed air from the cylinder chamber into the discharge manifold and receiver tank during the upward stroke. These valves open dynamically when the shifting internal cylinder pressure surpasses the pressure sustained within the discharge line. Because they are continuously subjected to peak mechanical forces and maximum thermal exposure, discharge valves are highly susceptible to carbonization and thermal fatigue.
Comprehensive Maintenance Protocols for Industrial Piston Valves
Optimizing valve longevity under demanding job site conditions requires a structured, multi-step engineering inspection routine:
1. Non-Destructive Visual Inspection
Regularly remove valve covers to inspect the valve discs, plates, and seats for micro-cracks, surface pitting, or localized distortion. In heavy-duty applications-such as pairing a compressor with a pneumatic jackhammer in a remote mine-pay close attention to the accumulation of hard carbon deposits or varnish on the sealing boundaries. Any brittle or compromised component must be replaced instantly to avert catastrophic cylinder drop-in.
2. Precision Chemical Cleansing
Accumulated carbon and oily sludge force valves to stick, destroying their timing and sealing geometry. Clean the valve components thoroughly using non-aggressive, specialized degreasing solvents and soft-bristled brass brushes. Avoid using harsh abrasives, steel wire wheels, or scrapers, as these can introduce microscopic scores on the precision-lapped seating surfaces, resulting in permanent high-pressure air leakage.
3. Dynamic Mechanical Adjustments
- Valve Clearance Calibration: Periodically verify the precise clearance tolerances between the valve stems and driving mechanisms according to original engineering blueprints. Deviant clearances alter the critical valve timing, choking air delivery.
- Spring Tension Verification: Valve springs must maintain uniform, calculated tension. Weakened springs lead to delayed valve closing and pressure blowback, while excessive tension induces accelerated mechanical impact wear on both the disc and seat faces.
Precision Installation and Environmental Alignment
The durability of a piston compressor valve is heavily influenced by the accuracy of its mechanical installation. During reassembly, maintenance crews must strictly adhere to the manufacturer's specified torque limits, utilizing cross-pattern tightening sequences to eliminate structural warping. Furthermore, correct axial alignment within the valve pocket is mandatory; minor angular misalignment generates uneven stress concentrations, causing premature reed fracturing.
Environmental factors must also be balanced. For instance, when operating heavy-duty equipment like our W-2.8/5 Diesel 15kw Belt Driven Piston Air Compressor in hot, high-humidity regions, installing high-efficiency oil-water separators and premium intake air filters is critical. This keeps the internal valve assemblies dry and free from abrasive airborne dust particles.
Troubleshooting Manifestations of Valve Malfunctions
Field operators should closely monitor the following operational indicators to diagnose underlying valve degradation before total system failure occurs:
- Degraded Volumetric Output: A visible drop in receiver tank pressure building speed or air flow rate is a primary indicator of back-leaking or broken valves.
- Abnormal Thermal Signatures: Defective valves cause compressed air to re-circulate within the cylinder, generating localized overheating. If a valve cover feels exceptionally hot to the touch, it indicates severe slippage or valve leakage.
- Acoustic Deviations: Listen for distinct knocking, metallic rattling, or persistent hissing sounds emanating from the cylinder head area, which point directly to loose components or cracked valve plates.
The "Moderate" Approach to Component Selection
At Moderate Machine, our engineering architecture is dictated by the philosophy of "Technical Balance" . We recognize that real-world operations do not require extreme, over-engineered designs that inflate capital expenditures, nor can they tolerate low-grade components that cause chronic field failures.
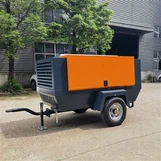
Our heavy-duty piston compressors-including the W-3.5/5 Mining Piston Type Air Compressor Head and the highly mobile W-1.8/5 Diesel Motor 11kw Mini Air Compressor-are purposefully designed with standard, highly compatible valve geometries that maximize component exchangeability and ensure stable operation under volatile mining and construction loads.
Conclusion
Securing the seamless, high-efficiency operation of a small piston air compressor relies heavily on the structural health of its intake and discharge valves. By implementing rigid inspection schedules, using correct cleaning solvents, and opting for high-durability, job-matched components, fleet managers can significantly mitigate maintenance overheads and extend the machine's lifetime operational yield.
Explore our W-3.5/5 Mining Piston Type Air Compressor
References
Compressor Handbook: A Guide to Compressor Technology and Applications, Industrial Engineering Press.
Reciprocating Piston Compressor Maintenance Manuals, Quzhou Zhongdu Machinery Quality Division.
ISO 1217:2012, Displacement compressors - Acceptance tests.